

Ball Valves, Control Valves, Lined Valves
Richter
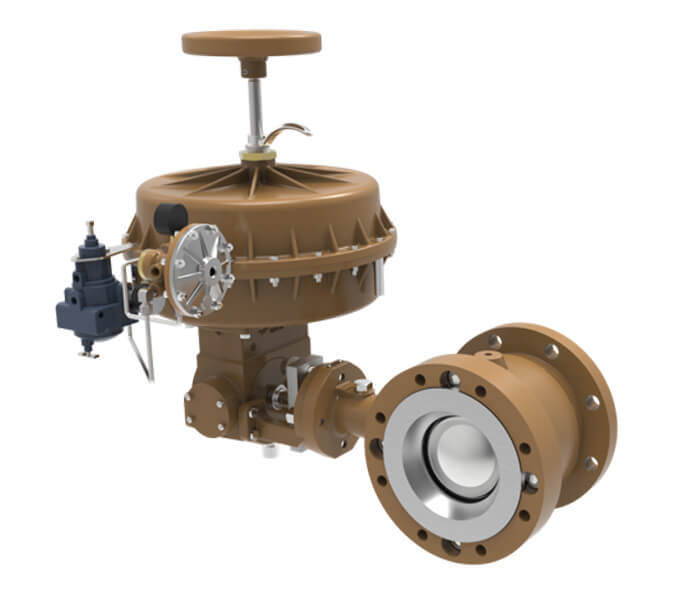
KNR PFA Lined Control Ball Valve
Includes
- BROCHURES
- IOM
- VIDEOS



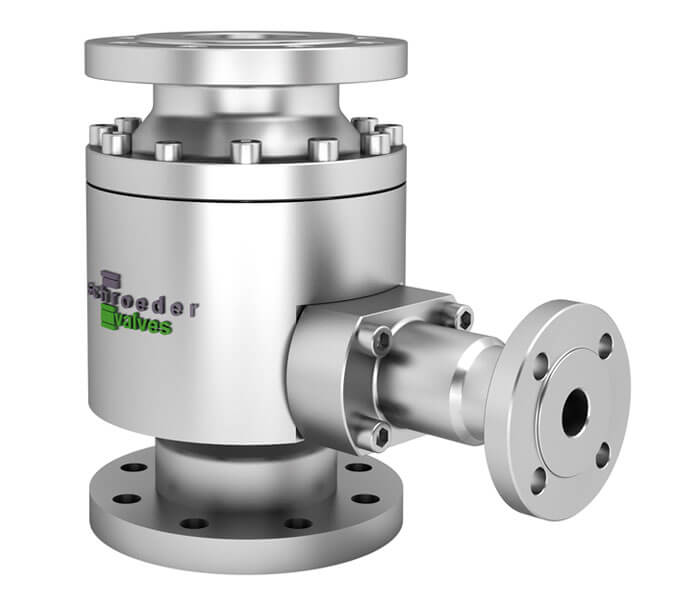
Pump Protection Valves
Schroeder
Schroeder SSV Automatic Recirculation Valve
Includes
- BROCHURES
- IOM
- VIDEOS


Applications
Chemical & Synthetic Fuels
Chemical and Synthetic Fuels Valve Solutions
Helping chemical and synthetic fuel plants improve uptime, protect critical equipment, and optimize process performance with proven valve and control solutions.
Chemical and synthetic fuel plants operate under some of the harshest process conditions found in industry. High temperatures, aggressive chemicals, erosive slurries, and fluctuating pressures place extreme demands on valves and control equipment.
At plants like Sasol's Secunda and Sasolburg facilities, achieving production targets depends on valves that deliver absolute reliability—providing tight shut-off, precise flow control, and critical pump protection across continuous and batch processes. Engineers and production managers rely on solutions that maximize uptime, reduce maintenance costs, and support safe, environmentally responsible operations.
At Valve & Automation, we supply valve and control solutions specifically selected to address the operational challenges faced in chemical and synthetic fuel plants. Our technologies are designed to reduce downtime, extend equipment life, and improve overall process efficiency—helping plants run safer, longer, and more profitably.
Zwick Tri-Con Triple Offset Valve
The Zwick Tri-Con is a precision-engineered triple offset valve delivering zero-leakage isolation in critical chemical and synthetic fuels applications. Its frictionless, cone-in-cone seating system ensures long-term sealing integrity under extreme pressure and temperature cycling.
Ideal for aggressive chemical services, steam isolation, and gas handling, the Zwick Tri-Con minimizes actuator loads, reduces maintenance, and extends valve life—supporting safer, more reliable plant operation.
Key Applications:
- Process steam and gas isolation
- High-temperature and high-pressure chemical services
- Emergency shut-down
Key Benefits:
- Zero-leakage, even under extreme conditions for maximum safety
- Longer seat life with frictionless seating
- Lower installation and maintenance costs due to lighter weight and compact design
Cashco Ranger QCT Rotary Globe Control Valve
The Cashco Ranger QCT is a high-performance rotary globe control valve engineered for rapid, precise response in challenging control applications. Its innovative quick-change trim design allows for 5-minute trim changes without removing the actuator, significantly reducing downtime during maintenance.
Suited for steam, slurry, chemical blending, and high-pressure drop services, the Ranger QCT provides tight, repeatable control to optimize process stability and throughput.
Key Applications:
- Steam and gas control
- Slurry and erosive chemical fluid control
- High-pressure drop chemical blending
Key Benefits:
- High control accuracy with minimal hysteresis
- Quick-change trim for fast maintenance and reduced downtime
- Long service life in abrasive and corrosive conditions
Schroeder SSV Automatic Recirculation Valve
The Schroeder SSV protects centrifugal pumps from damage caused by low or no-flow conditions by automatically ensuring minimum flow rates without external controls. Its compact design integrates a full-featured non-return valve, bypass flow control, and seat tightness into one rugged unit.
Essential for critical pump services across chemical and synthetic fuel plants, the SSV improves pump reliability, extends mean time between failures (MTBF), and reduces emergency shutdown risks.
Key Applications:
- Pump protection in chemical services
- Boiler feedwater pump protection
- Critical process pump safeguarding
Key Benefits:
- Protects pumps from minimum flow damage without external instrumentation
- Reduces unplanned shutdowns
- Compact, maintenance-free design
Partner with Valve & Automation
Our engineered valve and control solutions are trusted by leading chemical and synthetic fuel producers, including Sasol, to deliver high uptime, dependable performance, and efficient operation in the most demanding process environments.
We are committed to supporting Sasol and the broader chemical and synthetic fuels industry with proven technologies, responsive service, and solutions that drive long-term operational success.
- Browse the menu on the right for solutions on specific applications.
- Talk to our Technical Sales Specialists to find the best solution for your plant.

 Contact us Today - Tel: 0861 103 103
Mining & Minerals
Proven Valve & Control Solutions for the Mining & Minerals Industry
At Valve & Automation, we provide mining and mineral processing valve solutions—from manual isolation to advanced control—for demanding applications across extraction, separation, and refining. From abrasive slurry isolation to aggressive chemical dosing and precise process control, our valves are built for the tough conditions found in extraction, concentration, and refining.
We have a strong track record in high-value mineral refining environments, where zero leakage, chemical compatibility, and uptime are critical. Our Richter fully lined valves and pumps have delivered exceptional reliability in these applications—helping our clients reduce downtime, avoid safety incidents, and extend asset life.
Across platinum, gold, copper, and iron ore operations, we’ve helped plant teams with solutions that:
- Resist corrosion and abrasion in aggressive chemical and slurry services
- Provide accurate control in thickener underflow, flotation, and SX/EW processes
- Lower total cost of ownership by reducing maintenance and improving performance
- Enhance plant safety and environmental compliance
With technical specialists available to assist with valve sizing, material selection, and actuation, we ensure each valve is tailored to your process needs and plant conditions.
Explore Our Mining and Mineral Processing Valve Solutions
Richter Lined Valves & Pumps
Fluoropolymer-Lined for Corrosive Media
The Richter range of PTFE and PFA-lined valves and pumps is ideal for handling aggressive chemicals used in SX/EW, acid dosing, and high-purity refining. Designed to provide long-term corrosion protection and zero leakage, Richter valves offer safe, reliable performance in the most demanding chemical environments.
Key Applications:
- Sulphuric, hydrochloric, and hydrofluoric acid dosing
- Solvent extraction and electrowinning (SX/EW)
- High-purity metal refining
- Chemical containment in reagent prep and handling
Key Benefits:
- Superior chemical resistance with full fluoropolymer lining
- Zero-leakage sealing for maximum safety
- TA Luft-compliant for emissions control
- Available in ball, globe, diaphragm valves and lined centrifugal pumps
NAF-Setball SF – V-Port Ball Sector Control Valve
The NAF-Setball SF delivers precise flow control in tough slurry and chemical handling applications common to mineral processing plants. Its segmented ball design handles thickener underflow, flotation control, and chemical dosing with high accuracy and reliability—even in abrasive, solids-laden media.
Key Applications:
- Thickener underflow regulation
- Froth flotation control
- Chemical and pH reagent dosing
- Slurry flow metering
Key Benefits:
- High control accuracy, even at low flow rates
- Optional hard coatings for abrasive slurry resistance
- Low torque operation, reducing actuator stress
- Compact, short-pattern design simplifies installation
Stafsjö SLV – Fully Rubber-Lined Knife Gate Valve
Engineered for heavy-duty slurry isolation, the Stafsjö SLV features dual full-bore rubber sleeves that completely isolate internal components from abrasive media. Designed for harsh conditions found in tailings, cyclone feeds, and concentrate pipelines, it delivers consistent sealing with minimal maintenance.
Key Applications:
- Tailings and concentrate pipelines
- Cyclone feed isolation
- Thickener and clarifier underflow
- High-solids slurry service
Key Benefits:
- Full bore flow path reduces wear and pressure drop
- Self-cleaning sleeve design maintains sealing performance
- Long service life in abrasive slurry conditions
- Manual or automated actuation options available
Partner with Valve & Automation
Our engineered valve and control solutions are trusted by leading platinum, gold, copper, and iron ore producers to deliver plant reliability, process safety, and long-term performance in the most abrasive and chemically aggressive mining environments.
We are committed to supporting the Southern African mining and minerals industry with proven technologies, expert application support, and responsive service—helping operations reduce downtime, extend equipment life, and meet production targets with confidence.
- Browse the menu on the right for solutions on specific applications.
- Talk to our Technical Sales Specialists today to find the best solution for your plant.
Contact us Today - Tel: 0861 103 103
Oil & Gas
Oil & Gas Valve Solutions
Protecting Critical Equipment, Reducing Risk, and Maximizing Uptime Across Oil & Gas Operations
Valve & Automation helps oil and gas producers and processors—including Sasol, Sapref, Engen, Natref, Astron Energy, Vopak, and Bidvest Tank Terminals—maintain safe, efficient, and reliable operations under some of the harshest process conditions in industry. We supply proven valve and flow control technologies that stand up to aggressive media, extreme pressures, high temperatures, and volatile environments—where equipment failure can mean major safety and financial risks.
With trusted products from Zwick, Schroeder, and Cashco, we deliver solutions for high-integrity isolation, automatic pump protection, and explosion prevention across upstream, midstream, and downstream applications.
Zwick Tri-Con Triple Offset Valve
The Zwick Tri-Con is a precision-engineered triple offset valve delivering zero-leakage isolation in critical oil and gas services. Its frictionless, cone-in-cone seating system ensures long-term sealing integrity under extreme pressure fluctuations, temperature cycling, and corrosive service conditions.
Ideal for gas isolation, flare systems, steam services, and emergency shutdown, the Zwick Tri-Con minimizes actuator loads, reduces maintenance, and extends valve life—supporting safer, more reliable plant operation.
Key Applications:
- Gas and steam isolation
- Flare gas systems
- Emergency shutdown (ESD) services
- High-temperature and high-pressure oil and gas processes
Key Benefits:
- Zero-leakage sealing under extreme conditions for maximum process safety
- Longer seat and actuator life with frictionless cone-in-cone seating
- Lower installation and maintenance costs due to lightweight, compact design
Schroeder SSV Automatic Recirculation Valve
The Schroeder SSV is an automatic pump protection valve that safeguards centrifugal pumps against low-flow damage in critical oil and gas applications. It automatically ensures minimum flow without external power or instrumentation, offering a simple, highly reliable solution.
Perfect for condensate pumps, feedwater pumps, and hydrocarbon transfer pumps, the SSV helps prevent pump overheating, cavitation, and failure—reducing downtime and extending equipment life.
Key Applications:
- Centrifugal pump protection
- Condensate, feedwater, and hydrocarbon transfer services
- Process critical pumping systems in oil, gas, and refining plants
Key Benefits:
- Automatic, fail-safe pump protection with no external power or controls
- Compact, all-in-one valve design reduces piping and footprint
- Extended pump life and reduced maintenance costs
Cashco Flame Arrestors
Cashco flame arrestors provide essential protection against flame propagation in oil and gas facilities, helping prevent explosions and ensuring compliance with stringent safety and environmental standards. Their designs cover both deflagration and detonation arresting needs, offering robust protection in volatile vapor handling systems.
Commonly used in storage tanks, flare stacks, and vapor recovery systems, Cashco flame arrestors deliver trusted performance even in high-pressure and hazardous environments.
Key Applications:
- Storage tank vent protection
- Flare systems
- Vapor recovery units
- Pipeline and process vessel safety
Key Benefits:
- Proven explosion protection across a wide range of vapors and gases
- Compliance with API and international standards for safety
- Durable construction for harsh oil and gas environments
Partner with Valve & Automation
Our engineered valve and control solutions are trusted by leading oil and gas operators across Southern Africa—including Sasol, Sapref, Engen, Natref, Astron Energy, Vopak, and Bidvest Tank Terminals—to ensure high uptime, process safety, and reliable performance in some of the toughest operating conditions.
We are committed to supporting the oil and gas industry with proven technologies, responsive local service, and application-specific solutions that help reduce downtime, protect assets, and drive long-term operational success.
- Browse the menu on the right for solutions on specific applications.
- Talk to our Technical Sales Specialists to find the best solution for your plant.
Contact us Today - Tel: 0861 103 103
Power Generation
Power Generation Valve Solutions
Our power generation valve solutions help Eskom and other power stations improve uptime, protect steam systems, and reduce pump failures.
South Africa’s power generation industry operates under some of the most demanding service conditions—superheated steam, extreme pressure cycling, and corrosive condensate can all compromise plant reliability and safety if not properly controlled.
At major utilities like Eskom’s coal-fired power stations, valve failure is not an option. Turbine protection, steam isolation, and pump safeguarding are mission-critical. That’s why plants depend on high-integrity valve solutions that deliver tight shut-off, reliable flow control, and automatic pump protection across base-load and peaking operations.
At Valve & Automation, we supply valve and control technologies engineered for the unique challenges of power generation. Our products help plants reduce unplanned outages, extend equipment life, and run safely and efficiently under high-stress conditions.
HP Valves – High-Pressure Forged Valves
HP Valves are specifically designed for steam systems operating under extreme pressure and temperature. Manufactured from forged materials, these valves provide long-term durability in critical turbine and boiler circuits.
Ideal for main steam lines, turbine bypass, desuperheaters, and boiler feed systems, HP Valves offer outstanding resistance to thermal fatigue and pressure cycling—ensuring safe, consistent operation in base-load and peaking stations.
Key Applications:
- Superheated and saturated steam control
- Turbine bypass and venting
- Boiler feedwater systems
Key Benefits:
- Designed for long-term high-pressure/high-temperature service
- Forged construction for maximum reliability
- Supported locally for faster spares and service response
Zwick Tri-Con – Triple Offset Isolation Valve
The Zwick Tri-Con is a precision-engineered triple offset valve delivering zero-leakage steam isolation in critical power plant systems. Its metal-to-metal, cone-in-cone seating ensures reliable shut-off even during high-temperature cycling and thermal expansion.
Used extensively within Eskom, the Tri-Con helps improve plant safety, reduce valve changeouts, and simplify actuator sizing due to its low torque design.
Key Applications:
- Main and auxiliary steam isolation
- Condensate systems
- Emergency shut-down valves (ESDVs)
Key Benefits:
- Zero-leakage tight shut-off for steam and condensate isolation
- Frictionless seating extends service life
- Compact, lower-weight design for easier installation and maintenance
Schroeder SSV – Automatic Recirculation Valve
The Schroeder SSV protects centrifugal boiler feed pumps and condensate pumps by ensuring minimum flow conditions are always maintained—automatically, without external control systems.
Its integrated non-return valve and smart bypass function safeguard pumps during low-load conditions, reducing damage risk and improving pump life expectancy—especially important for load-cycling units.
Key Applications:
- Boiler feed pump protection
- Condensate pump safeguarding
- Minimum flow assurance in variable load conditions
Key Benefits:
- No external instrumentation needed—fully automatic
- Reduces cavitation and pump wear
- Compact and maintenance-free design
Partner with Valve & Automation
Our engineered valve and control solutions are trusted by Eskom and leading power producers across South Africa to deliver high uptime, system integrity, and safe operation in the most demanding power generation environments.
We are committed to supporting the power industry with proven technologies, responsive service, and engineered solutions that ensure long-term success—whether in large utility stations or smaller co-gen facilities.
- Browse the menu on the right for solutions on specific applications.
- Talk to our Technical Sales Specialists to find the best solution for your plant.
Contact us Today - Tel: 0861 103 103
pulp
No content available.
Pulp, Paper & Cellulose
Pulp, Paper & Cellulose Valve Solutions
The pulp, paper and cellulose industry is a harsh and challenging environment where equipment is constantly exposed to erosive slurries, corrosive chemicals, high temperatures, and vibrations from pumps and refiners. To ensure long-term reliability and safety, plants demand robust valve solutions that can handle these extreme conditions without compromising performance.
Valve & Automation offers application-specific valve and actuator solutions from leading manufacturers including NAF, Stafsjö, and Richter — trusted by local industry leaders such as Mondi, Sappi, and Mpact. These products are specifically engineered for continuous process stability, zero leakage, and reliable shut-off across the toughest applications in the mill.
Naf Process Valve Applications
Sugar
Sugar Industry Valve Solutions
Keeping Your Crushing Season Flowing — Reliable Isolation, On/Off, and Control Valves for Sugar Processing
The production of sugar for food, beverage, and industrial applications demands equipment capable of withstanding harsh process conditions. From handling steam, viscous and dirty media, chemicals, and solid sugar crystals, to managing erosive slurries, valves must perform reliably under constant load. In addition, many sugar mills also produce ethanol, further increasing demands on process equipment.
The extraction and refining processes in sugar production often operate under severe conditions, requiring uninterrupted performance during the critical crushing season. Technicians, engineers, and production managers rely on valves that deliver consistent isolation, on/off operation, and precise control to support maximum plant uptime, improved productivity, and meeting production targets.
At Valve & Automation, we supply valve and control solutions specifically selected to address the operational challenges faced in the sugar industry. Our products are engineered to support higher production targets, reduce downtime, and extend equipment life—keeping plants running reliably when it matters most.
NAF-Setball SF Ball Sector Control Valve
The NAF-Setball SF is a compact, high-performance V-port ball sector control valve designed for precise modulating service, even under the most demanding process conditions.
Ideal for steam, fibrous media, slurries, and utility services, it delivers exceptional control accuracy and long-term reliability—ensuring stable operation throughout the crushing season.
Key Applications:
- Steam control
- Slurry handling
- Utility services
Key Benefits:
- High control accuracy
- Compact, space-saving design
- Long service life even in erosive and fibrous media
Stafsjö MV Knife Gate Valve
The Stafsjö MV knife gate valve is engineered for reliable isolation, on/off, and control applications across dry and wet media. It excels in demanding services such as receivers and crystallisers, where media tends to dewater, solidify, or build up.
When fitted with a deflection cone, the Stafsjö MV redirects solid sugar crystals away from the seat towards the centre of the bore, significantly extending seat and gate life. This ensures reliable, uninterrupted service through even the most demanding crushing seasons.
Key Applications:
- Crystallisers and receivers
- Slurry, biomass, and ash handling
Key Benefits:
- Extended seat and gate life
- High reliability in media prone to build-up
- Robust performance under abrasive conditions
NAF-Torex High-Performance Butterfly Valve
The NAF-Torex high-performance butterfly valve offers exceptional versatility and reliability for critical sugar mill applications, including condensate, steam, and vacuum pan exhaust steam services.
Engineered for isolation, on/off, and modulating control duties, the NAF-Torex ensures precise, dependable performance across demanding process conditions.
As one of our best-selling valves, the NAF-Torex is stocked locally along with gearboxes, pneumatic actuators, and positioners to enable rapid assembly and fast delivery—helping plants minimize downtime and keep production moving.
Designed as part of a modular valve package system, the NAF-Torex reduces inventory requirements by fulfilling multiple roles, from manual shut-off to fully automated control, without the need for additional mounting brackets.
Key Applications:
- Condensate isolation and control
- Steam isolation and modulating
- Vacuum pan exhaust steam handling
Key Benefits:
- Rapid delivery from local stock
- Flexible modular design reduces inventory
- Long-term durability for high uptime operations
Partner with Valve & Automation
Our engineered valve and control solutions are trusted by leading sugar producers across Southern Africa to deliver high uptime, dependable performance, and efficient operation throughout the crushing season.
Talk to our Technical Sales Specialists today to find the best solution for your plant.
 Download the Sugar Industry Application Brochure
Contact us Today - Tel: 0861 103 103